How Does an Injection Screw Head Improve Plasticizing Performance in Injection Molding?
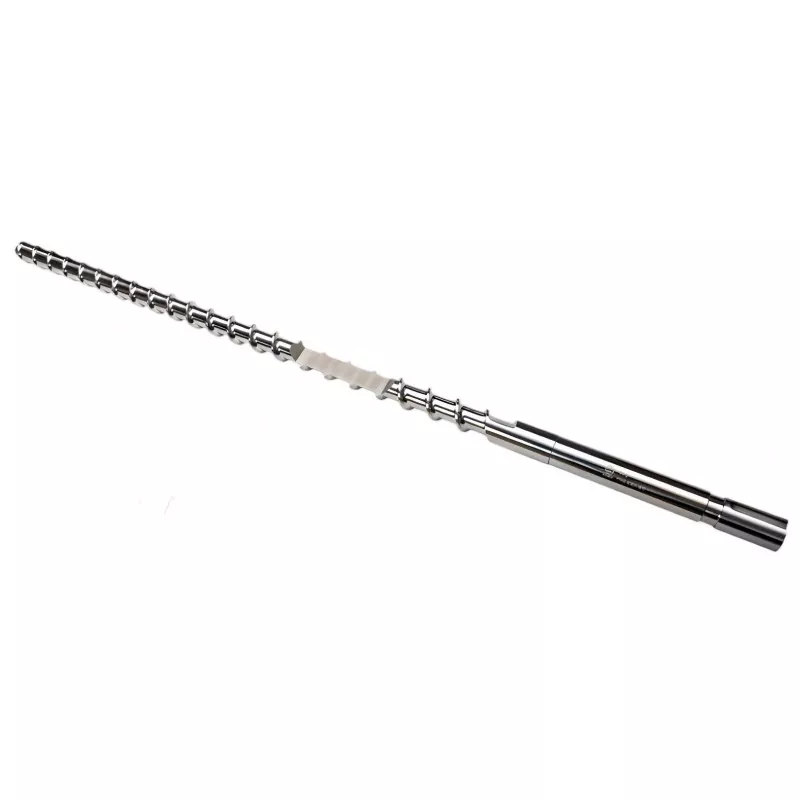
An injection screw head is a small but critical component of an injection molding screw assembly. It controls the flow of molten plastic during injection, helps prevent unwanted backflow during holding and injection stages, and contributes to consistent melt pressure and shot quality. When the screw head is incorrectly designed, poorly matched to the material, or worn beyond acceptable limits, manufacturers may experience unstable injection pressure, inconsistent shot weight, poor mixing, excessive material leakage, and increased production downtime. This guide explains the structure, working principle, material considerations, common problems, maintenance requirements, and selection criteria for injection screw heads, helping molding professionals make more informed decisions and improve machine reliability.

Table of Contents
- Why Is the Injection Screw Head So Important?
- What Is the Structure of an Injection Screw Head?
- How Does an Injection Screw Head Work?
- What Performance Problems Can a Poor Screw Head Cause?
- Which Materials Are Used for Injection Screw Heads?
- How Can Manufacturers Select the Right Injection Screw Head?
- What Causes Injection Screw Head Wear?
- How Can Injection Screw Head Service Life Be Extended?
- Injection Screw Head Design Considerations by Application
- Injection Screw Head Troubleshooting Guide
- Frequently Asked Questions
- Final Thoughts
Why Is the Injection Screw Head So Important?
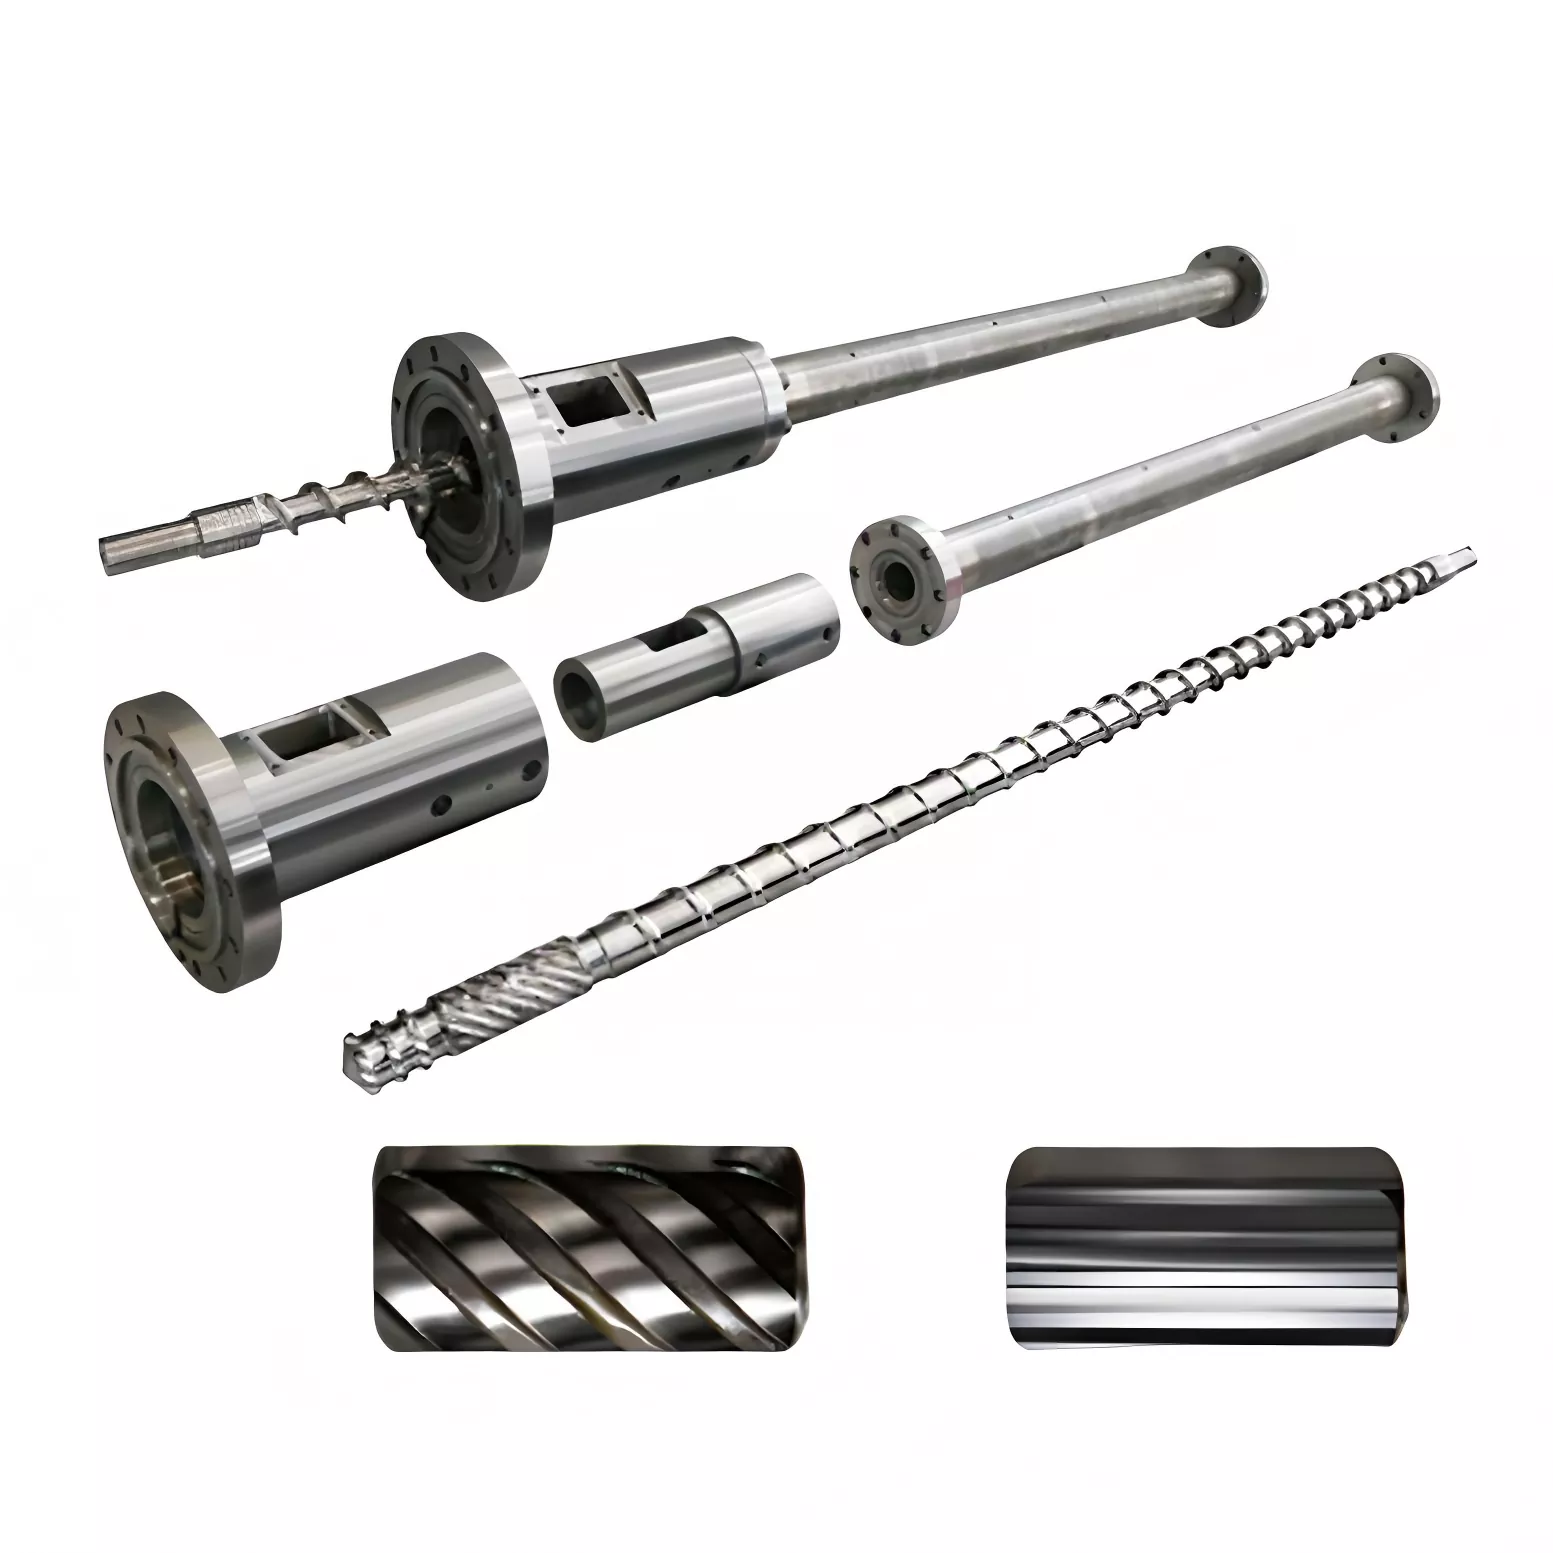
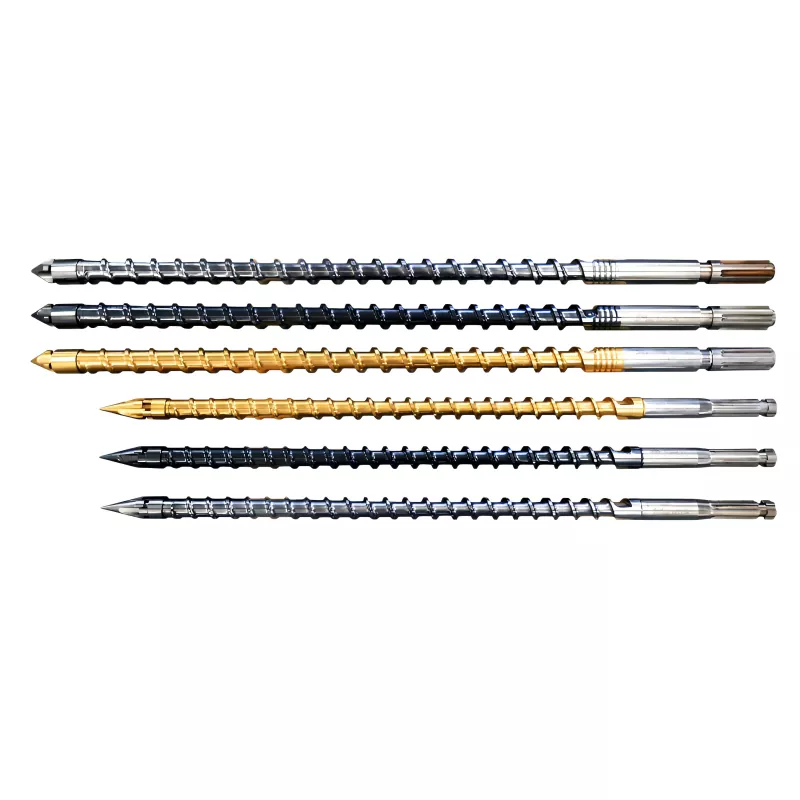
In an injection molding machine, the screw is responsible for conveying, melting, mixing, and injecting plastic material into a mold. While much attention is normally given to screw geometry, barrel condition, and heating systems, the injection screw head is equally important because it sits at the front end of the screw assembly and directly influences melt flow during injection and plasticizing.
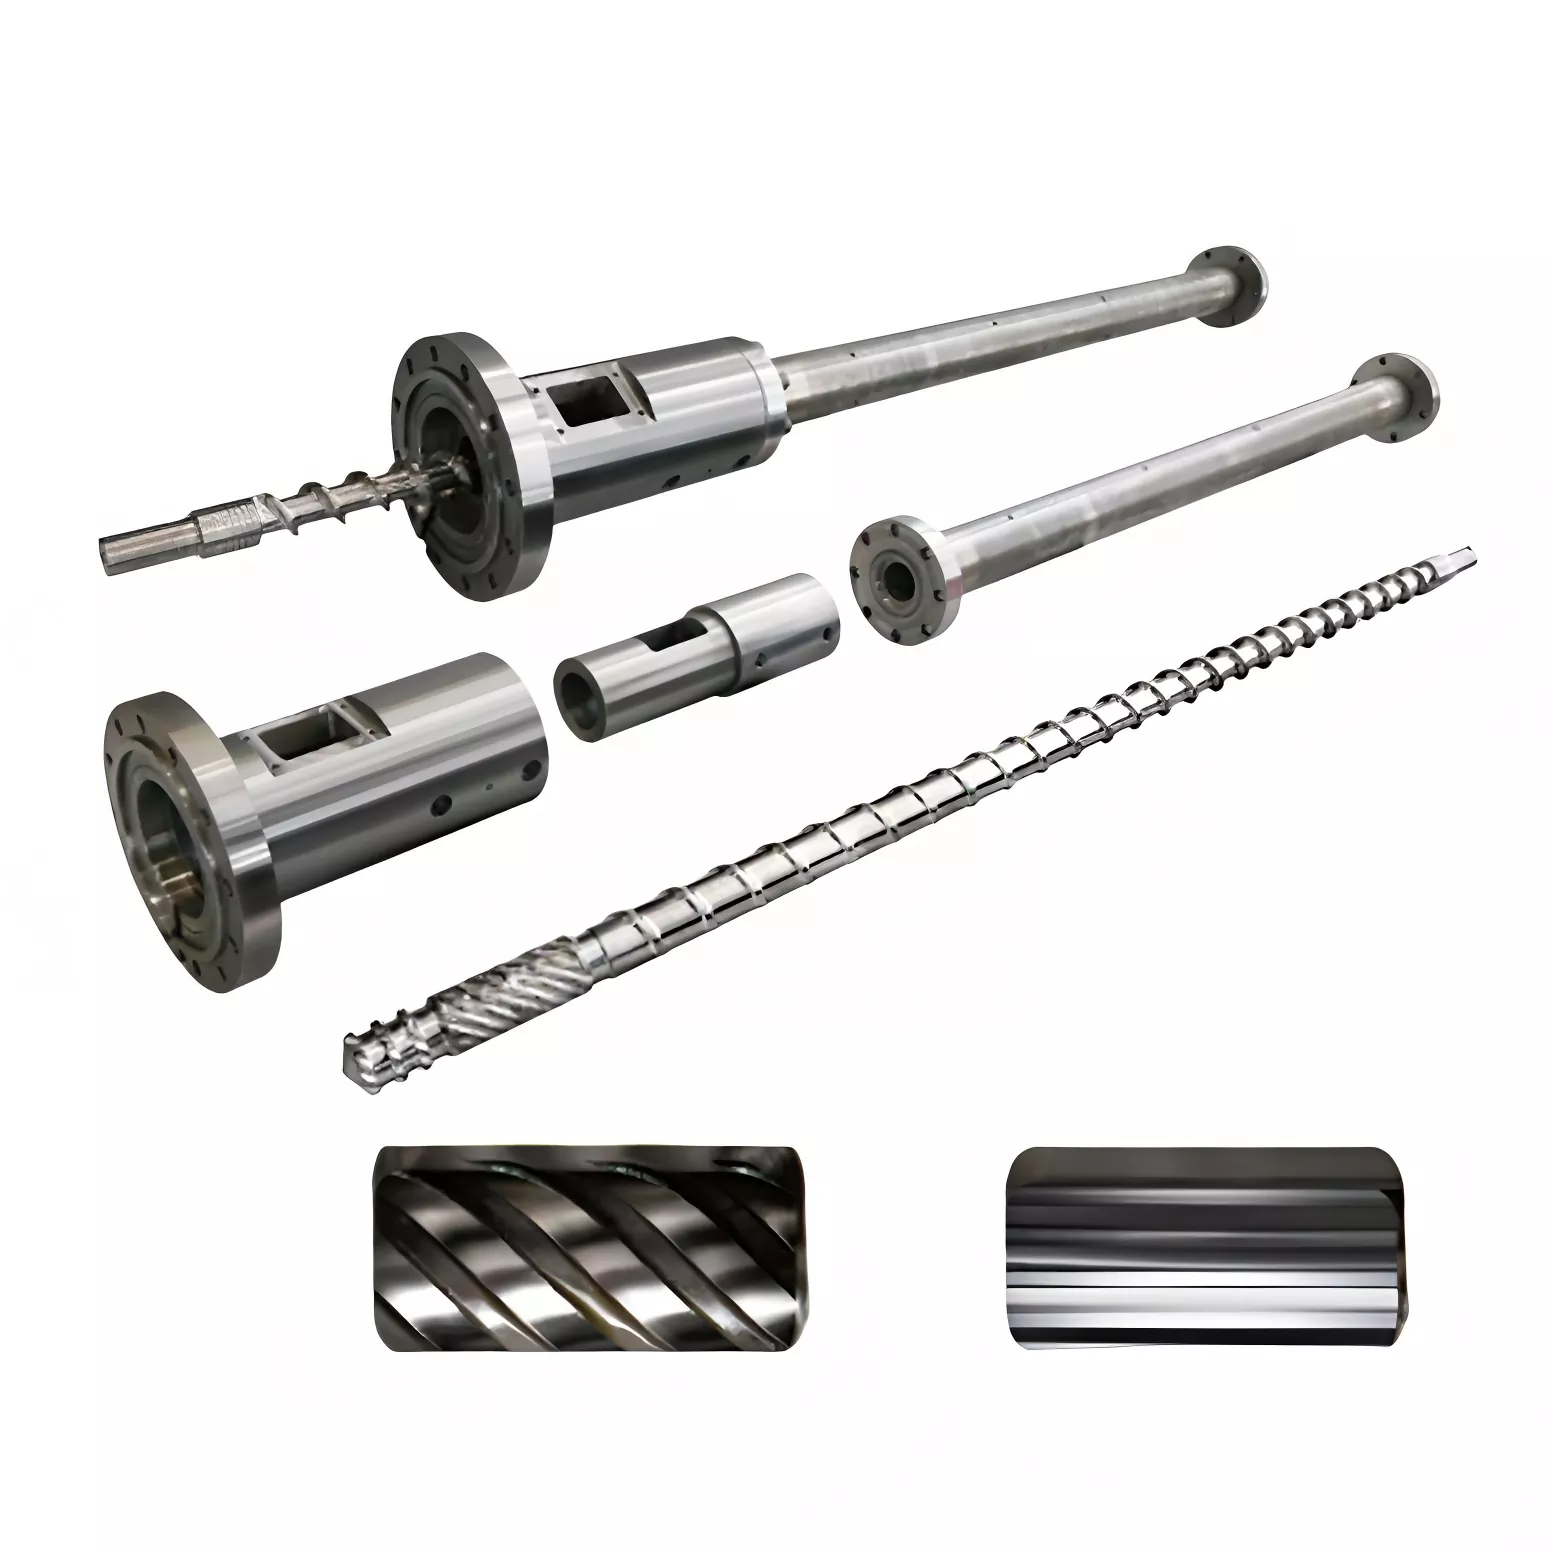
The screw head works together with components such as the check ring, thrust ring, and screw tip to create an effective non-return system. During plasticizing, the screw rotates and moves molten material toward the front of the barrel. During injection, the screw moves forward and the screw head assembly helps control the molten polymer so that the material is delivered into the mold with predictable pressure and volume.
A properly designed screw head can contribute to:
- More stable injection pressure
- Better shot-to-shot repeatability
- Reduced melt backflow
- More consistent shot weight
- Improved plasticizing efficiency
- Better control of molten material
- Reduced material leakage around the check ring
- Lower risk of premature component failure
For manufacturers producing precision components, packaging products, automotive parts, medical products, household items, or technical plastic components, these advantages can directly influence product quality and manufacturing costs.
What Is the Structure of an Injection Screw Head?
An injection screw head is not simply a single piece of metal. Depending on machine design and application requirements, the front-end assembly may contain several coordinated components. Their dimensions, surface condition, material, and tolerances must work together to maintain controlled melt movement.
| Component | Primary Function | Importance |
|---|---|---|
| Screw Head / Screw Tip | Connects the front of the screw to the non-return assembly and guides melt flow | High |
| Check Ring | Helps limit backward movement of molten plastic during injection | Very High |
| Thrust Ring | Supports the check ring and contributes to assembly stability | High |
| Sealing Surfaces | Help reduce uncontrolled material leakage | High |
| Threaded Connection | Secures the front-end components to the screw | High |
The exact configuration varies according to injection machine type, screw diameter, screw design, polymer characteristics, and production requirements. Therefore, replacing a screw head based only on external appearance is not recommended. Dimensional compatibility and application conditions must be evaluated together.
How Does an Injection Screw Head Work?
The injection cycle can be simplified into several stages, and the role of the screw head changes throughout the process.
1. Plasticizing Stage
During plasticizing, the screw rotates inside the heated barrel. Plastic pellets are transported forward while heat and mechanical shear transform the solid material into a molten state.
As molten plastic accumulates in front of the screw, the screw moves backward to create the required shot volume. The screw head and check-ring assembly must allow melt to move forward efficiently while maintaining appropriate sealing behavior.
2. Injection Stage
When injection begins, the screw stops rotating and moves forward. The screw head assembly works with the check ring to reduce reverse movement of the melt.
If excessive backflow occurs, the actual amount of material entering the mold can differ from the intended shot volume. This may result in inconsistent filling, variations in part weight, dimensional instability, or short shots.
3. Holding Pressure Stage
After the cavity is filled, holding pressure is applied to compensate for polymer shrinkage. The screw head assembly needs to maintain stable melt control during this stage.
A worn or poorly matched non-return system may cause pressure loss. In demanding applications, even relatively small variations can become visible as differences in product dimensions or weight.
4. Recovery Stage
After injection and holding, the screw rotates again to prepare the next shot. The screw head assembly returns to its plasticizing function, allowing the system to repeat the cycle.
This repeated movement means the screw head can experience substantial mechanical and thermal stress over the course of long production runs.
What Performance Problems Can a Poor Screw Head Cause?
When an injection screw head does not match the machine or material, production problems may appear gradually rather than immediately. This makes accurate diagnosis particularly important.
| Observed Problem | Possible Screw Head Issue | Potential Production Effect |
|---|---|---|
| Unstable shot weight | Check-ring leakage or excessive clearance | Variable product weight |
| Injection pressure fluctuation | Inconsistent sealing or wear | Unstable filling conditions |
| Longer recovery time | Incorrect flow characteristics or wear | Lower productivity |
| Material leakage | Damaged sealing surfaces | Material waste and pressure loss |
| Incomplete filling | Backflow or inadequate melt control | Short shots or defects |
| Black specks or contamination | Surface damage or degraded material accumulation | Appearance defects |
It is important to avoid immediately blaming the screw head for every molding problem. Barrel temperature, screw speed, back pressure, material moisture, mold condition, injection speed, and machine control parameters can also produce similar symptoms. A systematic inspection is therefore more reliable than changing components based on a single symptom.
Which Materials Are Used for Injection Screw Heads?
Material selection has a major influence on the working life of an injection screw head. Different polymers create different levels of abrasion, corrosion, heat exposure, and mechanical stress.
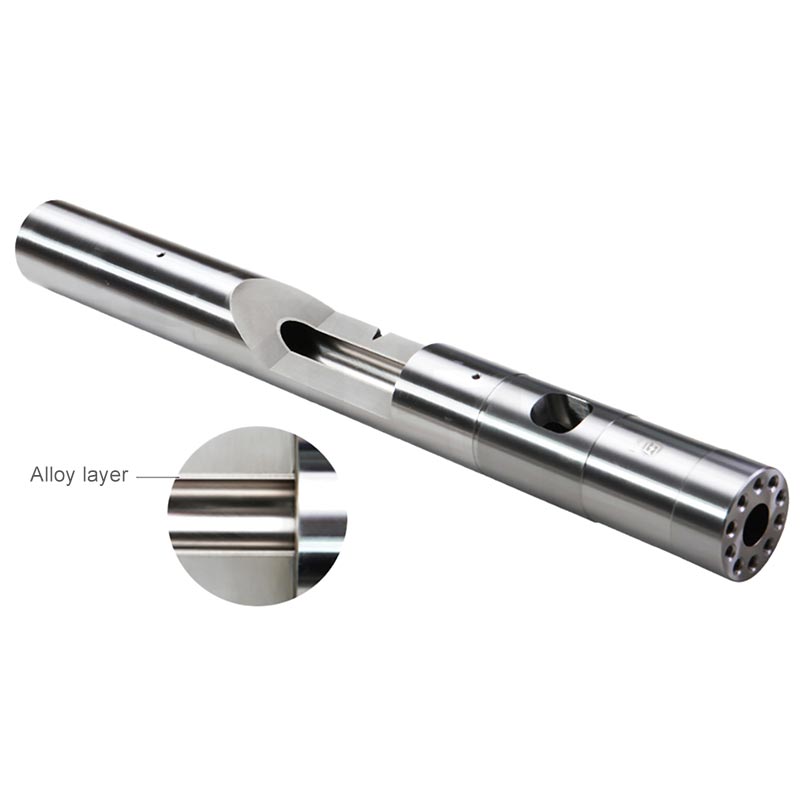
Common engineering approaches include the use of alloy steels with suitable heat treatment, nitrided surfaces, hardened components, or specialized wear-resistant materials for demanding applications.
| Material / Treatment Approach | Typical Advantage | Potential Application |
|---|---|---|
| Alloy Steel | Good strength and machinability | General injection molding |
| Nitrided Steel | Improved surface hardness and wear resistance | Standard and moderately abrasive materials |
| Hardened Steel | Higher resistance to mechanical wear | Long-running production |
| Corrosion-Resistant Materials | Better resistance to corrosive polymers | PVC and chemically aggressive applications |
| Special Wear-Resistant Alloys | Enhanced resistance to severe abrasion | Glass-filled or mineral-filled polymers |
Materials containing glass fiber, mineral fillers, flame retardants, or other additives can accelerate component wear. In these cases, a standard screw head may not provide the desired service life.
How Can Manufacturers Select the Right Injection Screw Head?
Selecting an injection screw head should begin with the actual operating conditions rather than simply the machine brand or screw diameter.
Key factors include:
- Machine specifications: Confirm screw diameter, barrel dimensions, connection dimensions, and front-end assembly requirements.
- Plastic material: Identify whether the polymer is standard, engineering-grade, filled, reinforced, corrosive, or highly abrasive.
- Production volume: High-volume continuous molding places greater demands on wear resistance and dimensional stability.
- Injection pressure: Higher-pressure applications require components with suitable mechanical strength and dimensional accuracy.
- Temperature: Processing temperature affects thermal stress and material behavior.
- Shot size: The screw head must be appropriate for the machine's actual injection requirements.
- Maintenance history: Previous wear patterns can provide valuable information when selecting a replacement.
- Required service life: A low-cost component is not necessarily economical if frequent replacement causes production downtime.
A reliable supplier should be able to review drawings, dimensions, machine information, material specifications, and operating conditions before recommending a component.
What Causes Injection Screw Head Wear?
Wear is one of the most common reasons for injection screw head replacement. However, the rate of wear can vary dramatically between applications.
Material Abrasion
Glass-filled plastics and mineral-filled polymers can be significantly more abrasive than conventional polypropylene or polyethylene. Continuous processing can gradually damage critical surfaces.
Corrosion
Some polymers, additives, and processing conditions can create corrosive environments. Corrosion may affect sealing surfaces and dimensional accuracy.
Excessive Temperature
Operating outside the recommended temperature range can accelerate material degradation and may increase thermal stress on the screw assembly.
Improper Assembly
Incorrect installation, inadequate cleaning, damaged threads, or incorrect tightening can create uneven loading and premature component damage.
Insufficient Maintenance
Residue buildup can interfere with component movement and sealing. Regular inspection is particularly important for machines running continuously or processing abrasive materials.
How Can Injection Screw Head Service Life Be Extended?
Preventive maintenance is generally more cost-effective than waiting for severe wear to affect production.
- Inspect the screw head and check-ring assembly at scheduled intervals.
- Measure critical dimensions instead of relying only on visual inspection.
- Clean polymer residue during planned maintenance.
- Check sealing surfaces for scoring, pitting, or abnormal wear.
- Inspect threads and connection areas for damage.
- Monitor changes in injection pressure and shot weight.
- Record recovery time and molding-cycle changes.
- Pay special attention to glass-filled and other abrasive materials.
- Use appropriate installation procedures when replacing components.
- Keep records of component replacement and operating conditions.
One of the most useful maintenance indicators is a gradual change in molding consistency. If the machine previously produced stable shot weights but begins showing increasing variation, the screw and non-return assembly should be included in the inspection process.
Injection Screw Head Design Considerations by Application
There is no single screw head configuration that is ideal for every injection molding application. Production requirements can vary considerably.
| Application | Main Challenge | Important Consideration |
|---|---|---|
| Commodity Plastics | High production volume | Reliable sealing and economical service life |
| Engineering Plastics | Higher processing temperatures | Thermal stability and dimensional accuracy |
| Glass-Filled Plastics | High abrasion | Enhanced wear resistance |
| PVC Processing | Corrosive processing environment | Appropriate corrosion-resistant materials |
| Precision Components | Strict shot-to-shot consistency | Accurate dimensions and stable sealing |
| High-Volume Production | Long continuous operating time | Durability and predictable maintenance intervals |
This is why experienced component manufacturers normally consider the complete operating environment rather than treating the screw head as an isolated replacement part.
Injection Screw Head Troubleshooting Guide
When molding quality suddenly changes, the following diagnostic sequence can help narrow down the problem.
- Check shot-weight variation. Compare several consecutive molded parts.
- Review injection pressure. Look for unusual pressure changes under otherwise stable conditions.
- Check recovery behavior. An unexpected increase in recovery time can indicate changes in plasticizing performance.
- Inspect the non-return assembly. Look for wear, scoring, deformation, or material buildup.
- Measure critical clearances. Do not rely exclusively on visual inspection.
- Review material conditions. Check whether the resin or additives have recently changed.
- Review processing parameters. Confirm temperature, screw speed, back pressure, and injection settings.
- Compare historical maintenance records. Previous wear patterns can reveal recurring issues.
If the same problem continues after process parameters have been verified, a detailed inspection of the screw, barrel, screw head, and check-ring assembly is recommended.
Frequently Asked Questions
What is an injection screw head?
An injection screw head is the front-end component of an injection molding screw assembly. It works with the check-ring and related components to manage molten plastic flow during plasticizing, injection, and holding-pressure stages.
Why does an injection screw head wear out?
Common causes include abrasive plastics, glass fibers, mineral fillers, corrosive materials, high temperatures, improper assembly, insufficient maintenance, and long operating cycles.
How do I know when an injection screw head needs replacement?
Warning signs can include unstable shot weight, injection pressure fluctuations, increased material backflow, inconsistent molding quality, abnormal recovery behavior, visible surface damage, and excessive component clearance. Dimensional measurement should be used to confirm wear whenever possible.
Can an injection screw head be customized?
Yes. Screw heads can be manufactured according to machine specifications, drawings, dimensions, material requirements, processing conditions, and application needs. Customization can be especially useful when a standard replacement does not provide sufficient wear resistance or dimensional compatibility.
Are screw heads for abrasive plastics different?
They may require different material selection, heat treatment, surface treatment, or design considerations. Glass-filled and mineral-filled polymers can cause substantially greater wear than many unfilled plastics.
Does the screw head affect shot consistency?
Yes. The screw head and non-return assembly influence how effectively molten plastic is controlled during injection. Excessive leakage or wear can contribute to shot-weight variation and inconsistent molding conditions.
How often should an injection screw head be inspected?
There is no universal inspection interval because wear depends on material, temperature, production volume, machine design, and operating conditions. High-volume or abrasive applications generally require more frequent inspection.
What information should be provided when ordering a replacement?
Useful information includes machine model, screw diameter, screw drawing, screw head dimensions, plastic material, additives or fillers, processing temperature, production application, and any known wear problems. Providing accurate technical information helps reduce compatibility risks.
Final Thoughts
The injection screw head may be a relatively compact component, but its influence on injection molding stability is significant. Proper screw head design and maintenance can help control molten plastic, reduce backflow, support consistent shot weight, and improve the reliability of the overall injection system.
For manufacturers experiencing unstable shot weight, pressure fluctuations, premature wear, or recurring molding defects, the screw head and check-ring assembly deserve careful attention. Instead of replacing components based solely on appearance or price, it is better to evaluate machine dimensions, polymer characteristics, processing conditions, wear patterns, and expected production life together.
ZHOUSHAN HAPPY PLASTICS MACHINERY CO., LTD. focuses on plastic machinery components and can provide technical support for customers seeking suitable injection screw head solutions. Whether you need a standard replacement, a wear-resistant solution, or a component manufactured according to specific drawings and application requirements, selecting the right configuration can help reduce unexpected downtime and improve long-term production stability.
Need a reliable injection screw head for your molding machine? Contact ZHOUSHAN HAPPY PLASTICS MACHINERY CO., LTD. with your machine model, screw dimensions, material information, drawings, or application requirements. Our team can help evaluate the appropriate solution and provide professional assistance for your injection molding project.
Previous :
-
Related News
- How Does an Inject Mold Screw Barrel Improve Injection Molding Performance?
- How Does Injection Machines Bimetallic Screw Improve Plastic Processing Performance?
- How Does a Barrel for Chen Hsong Injection Machine Improve Injection Molding Performance?
- What Makes Barrel for YIZUMI Injection Machine Essential for Better Plastic Manufacturing Performance?
- What Makes Plastic Injection Screw And Barrel Essential for High-Performance Plastic Processing?
- What Is an Extruder Gearbox and How Does It Work in Plastic Processing?
Leave me a message